pause after pre-pierce when cutting stainless steel
Andrew Burdon21 days ago5 comments
when piercing thick stainless steel plate. (6pl and above) the amount of dross that is deposited on the surface causes a torch collision.
the solution is to pre-piece all the holes and lead-ins for the whole job fist, then have the machine pause before starting the cutting.
this allows the dross to be cleaned off, once clean you can hit a continue button to continue cutting the job.
is it possible for you add a 'torch blow through' option that can be turned on or off before generating the g-code.
(on some jobs i would have 300+ pierces that would need cleaning off, which is why it would be good to do all the piercing first)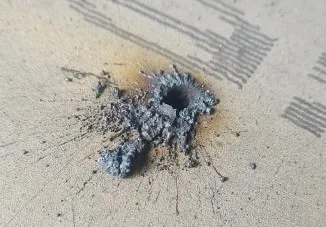
Regards.
Andrew
dross on 10pl stainless.jpg
5 Comments
Hello Andrew,
That's a great idea. I can add a checkbox in Plasma->Parameters->Cut for "Pre-Pierce" that can do just that. It will pierce all first then park the torch with a comment telling you to clear pierce dross then continue will start the program run. Since all the pierces are already made, I think we'll have to over-ride the arc okay signal on each touchoff in a pre-peircing program though. I'll test that with my Hypertherm unit and I'll possibly add an option to toggle that behavior. I can have this in the next release, let me know if that configuration sounds good to you
Thanks,
Travis Gillin
thank you, that sound perfect.
If the arc ok signal is an issue, shifting the whole cutting geometry in the Y direction by half the pierce hole diameter usually works. this allows the torch to "find" the plate again, rather than finding nothing where the pierce hole is. the slight geometry movement usually does not cause any issues.
i have done this manually when cutting 32pl stainless steel, because the pre-pierce holes are so large the torch can't find the plate to establish an arc.
my process sequence (with our old cutting software) used to be - pre-pierce all holes and lead-ins - pause - clean dross off - shift the machines origin 2mm in the Y direction (across the cutting bed) - press the continue button again.
You're welcome! That's a good idea. I think I'm going to pierce in all the original pierce points then shift the cut starts after all the pierces are done just along the original direction of the cut path, essentially what you suggested. I'm hoping to have the next release by the end of the week or this weekend, a whole bunch of new drafting features have been built and lots of bug fixes.
Travis
Thanks for the update.
can't wait to give it a try.
Hello Andrew,
I wanted to reach out and see if you're happy with the pierce all feature I rolled out in the last update to address this feature request. If there's anything you find off or something else that would make things better with this, let me know here.
Additionally, since you've been using JC3 for a little while now, I'm going to send you a link to review to the email address on your account. There's no obligation to submit a review but if you're happy with the software and want to help me grow this system, it would be much appreciated! I'm looking forward to seeing more feature requests from you in the future! Thank again.
Sign in to leave a comment or vote.
Sign In